Blog
87° elbow pipe fitting mould
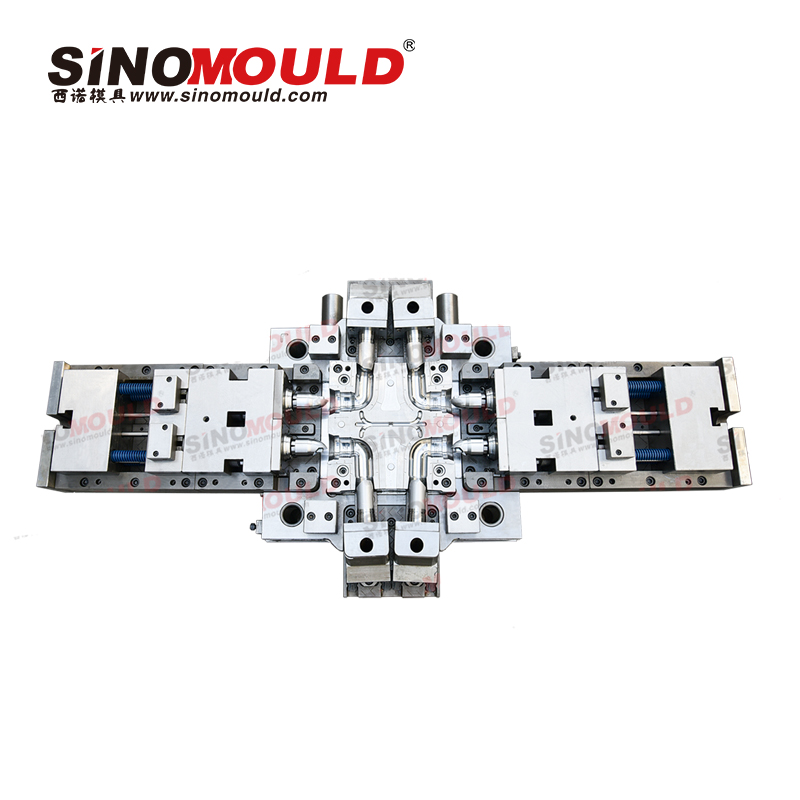
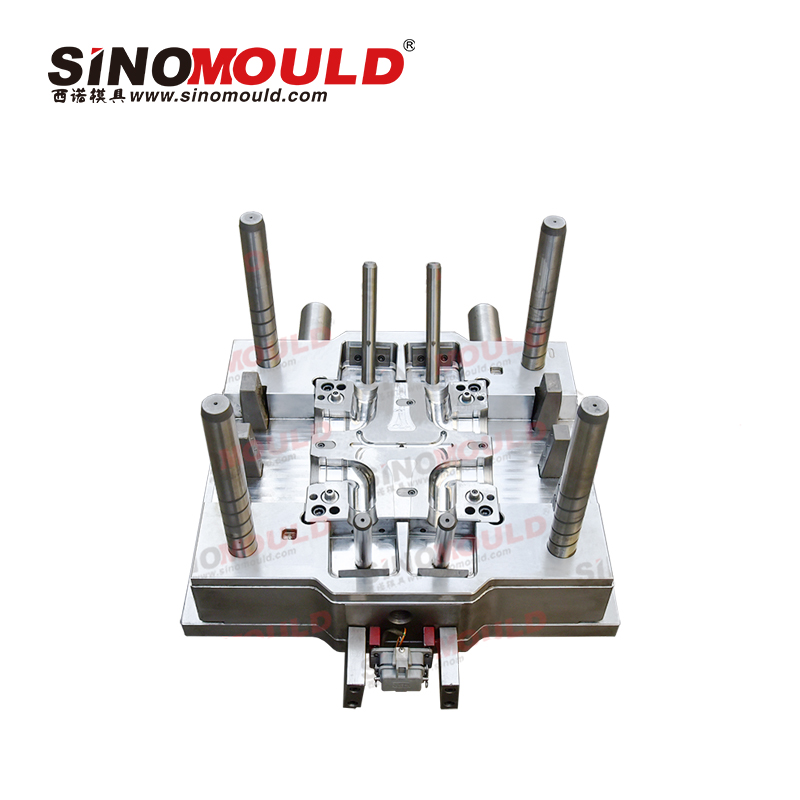
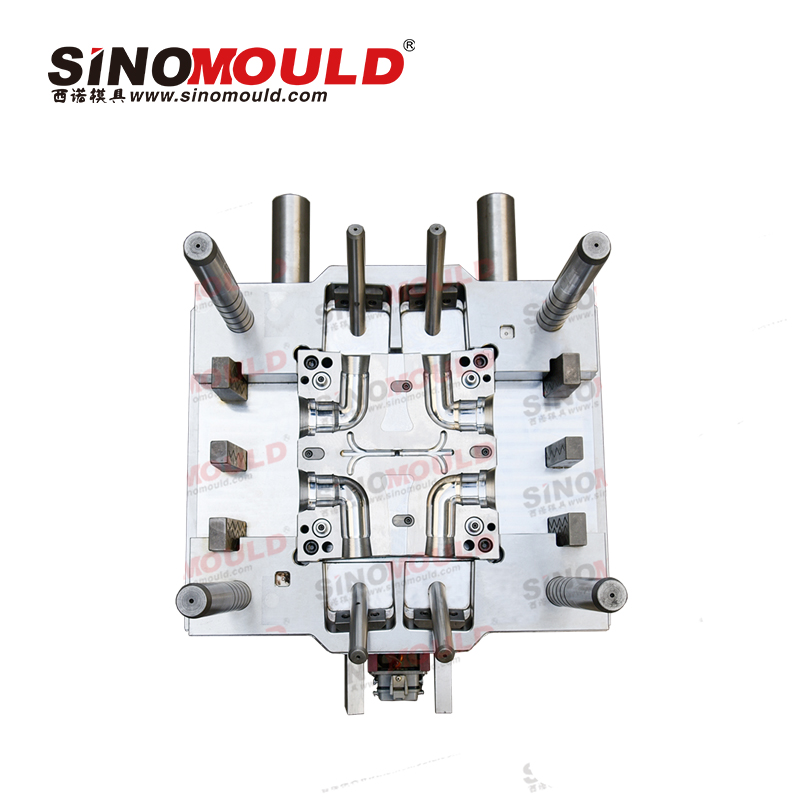
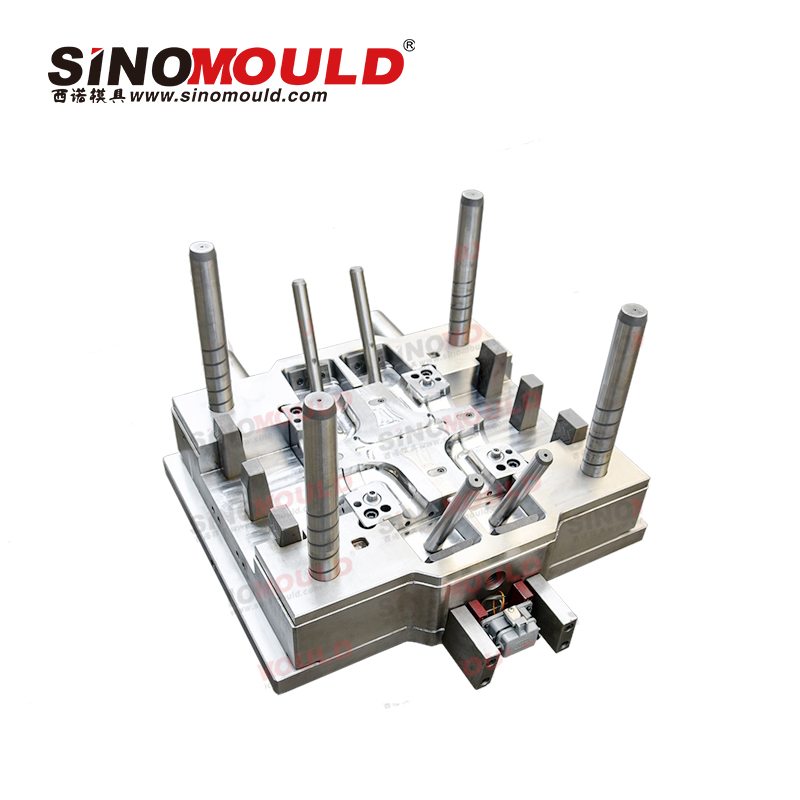
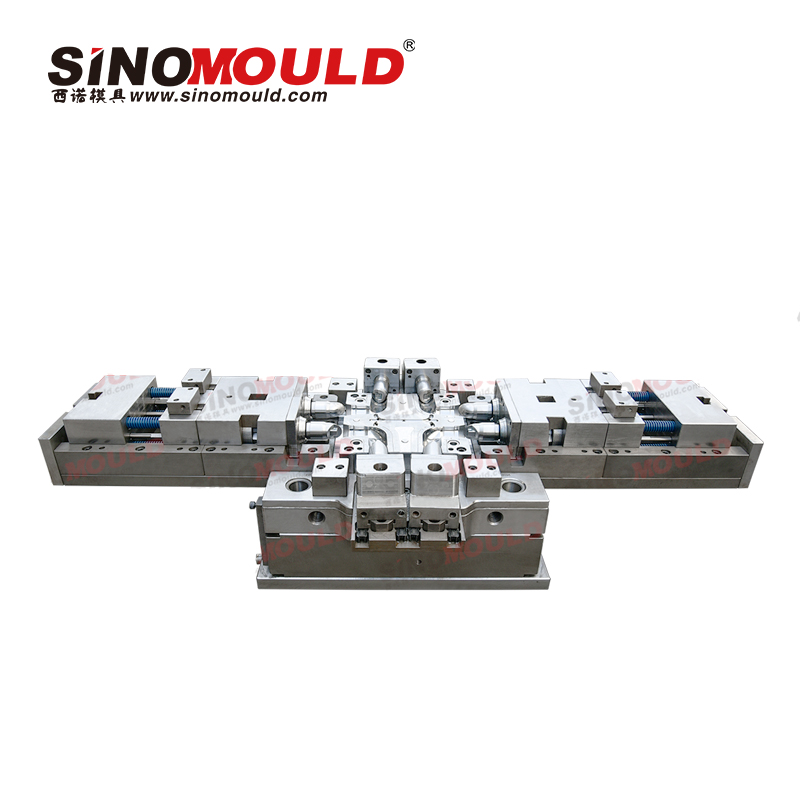
The 87° elbow pipe fitting mould is a specialized injection mould for elbow connectors used in water supply, drainage and chemical piping systems. Sino Mould customizes 87° elbow pipe fitting mould of different sizes, compatible with PVC, PPR, HDPE and other pipe materials. This 87° elbow pipe fitting mould adopts side core pulling slider structure to solve the undercut demolding difficulty of curved elbow parts. Uniform cooling channels are arranged inside the mould to guarantee precise bending angle and consistent wall thickness of finished elbows for stable mass production. With rich experience in pipe fitting mould manufacturing, we provide one-stop service including 3D design, mold flow analysis, machining, sample trial and after-sales maintenance.
Parameters of 87° elbow pipe fitting mould
Below are examples of the most common parameters for 87° elbow pipe fitting mould
| Mould Cavity Steel | DIN 1.2316, S136, 718H | Recommended Injection Machine | 350T – 800T |
|---|---|---|---|
| Mould Core Steel | DIN 1.2316, S136, P20 | Plastic Material | PVC (rigid / lead-free), PP, PE |
| Mould Base Standard / Steel | LKM Standard / S50C, S45C | Ejection System | Ejector plate + evenly distributed pins |
| Sliders, Inserts, Lifters Steel | High-strength tool steel, nitrided | Injection Process | Precision injection, mould temperature control ±2°C |
| Number of Cavities | 1 cavitie,2 cav,4 cav | Injection Cycle Time | 50-90 seconds |
| Hot Runner System | Hot runner + localised cold runner (PVC-specific) | Mould Manufacturing Lead Time | 45–70 days |
Quality points of 87° elbow pipe fitting mould
The key quality targets of the 87° elbow pipe fitting mould focus on bending angle accuracy, inner dimension, socket sealing performance, anti-sticking and flash control.
- Angle tolerance control: The positioning stroke of side sliders must be accurate, to keep the finished elbow steadily at 87°, avoid leakage risk caused by angle deviation in bulk production.
- Balanced cooling: Curved elbow area tends to overheat. Profiled cooling channels follow the elbow curve to reduce warpage, sink marks and weld lines.
- Sealing socket surface: High polish on the sealing zone, no tool marks or pits, to ensure tight connection between pipe fittings.
- Slider locking mechanism: Anti-backward locking blocks are installed to prevent slider retreat under high injection pressure and eliminate flash.
- Corrosion resistance: S136 steel is preferred for PVC processing to resist corrosion from decomposed PVC melt and extend the service life of the 87° elbow pipe fitting mould
Machining points of 87° elbow pipe fitting mould
The machining difficulty of 87° elbow pipe fitting mould lies in curved cavity surface and special-shaped slider, requiring strict control over CNC, EDM and polishing:
- Run Moldflow simulation at the early design stage to predict weld lines and air traps, optimize gate position and vent slots in advance.
- Fine CNC machining for curved cavity and core with proper polishing allowance; 5-axis machining for smooth curved surface.
- Precision grinding on slider mating and sliding surface, to guarantee smooth core pulling without jamming, with tight clearance control.
- Vent slot depth adjusted according to raw material. For PVC, vent depth ≤0.02mm to prevent flash.