Blog
5ml Syringe Plunger Mould
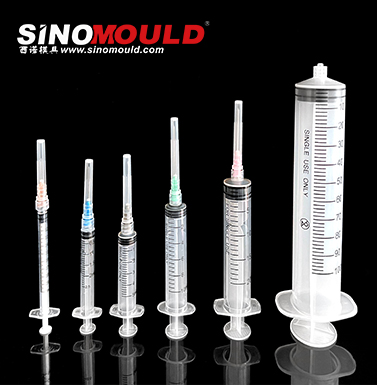
The 5ml syringe plunger is a slim medical component, assembled with barrel and rubber gasket to deliver liquid medication. It demands high concentricity, smooth rod surface and precise head flatness for smooth sliding without jamming or burrs. Medical-grade PP is commonly used, offering chemical inertness and compatibility with EO/gamma sterilization.
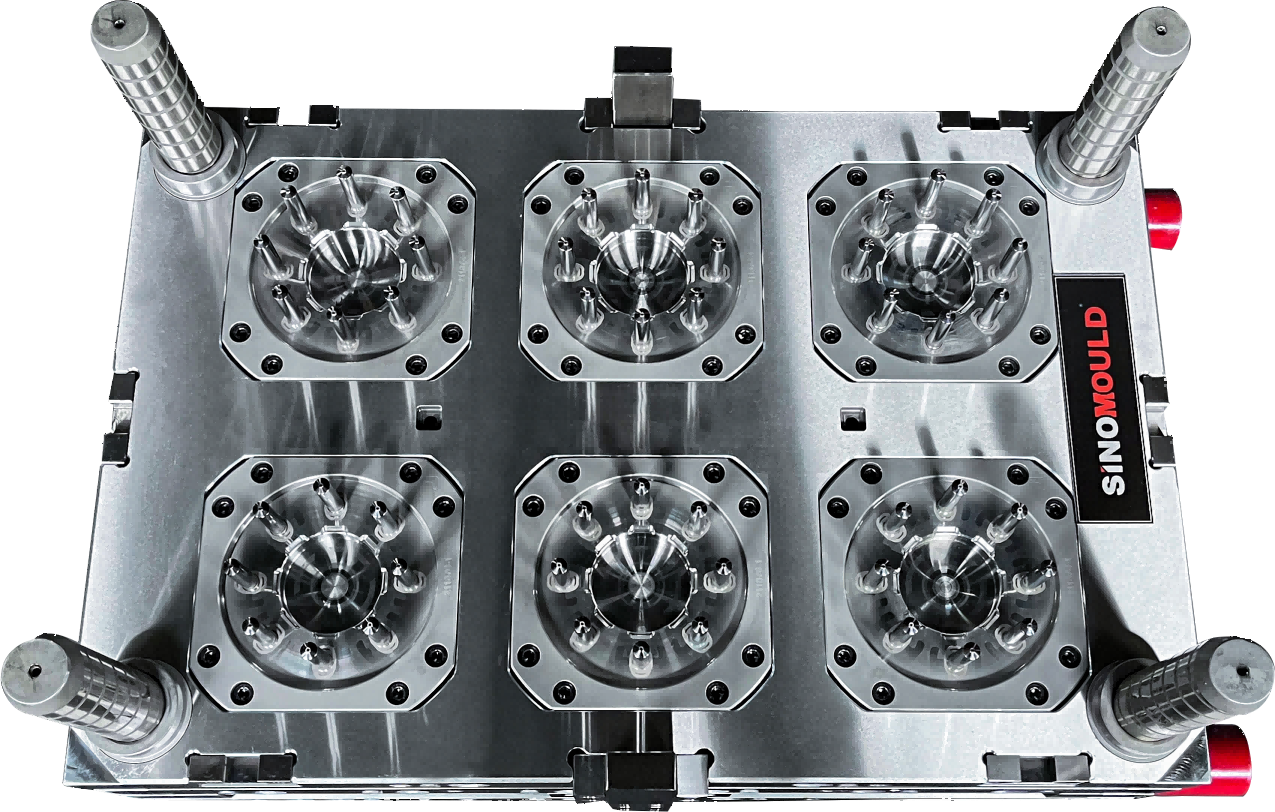
5ml Syringe Plunger Mould Details
5ml Syringe Plunger Mould Details
Moulding difficulties mainly include slender core deflection, concentricity deviation and PP uneven shrinkage, as even tiny flash may scratch the gasket. At SINOMOULD, we leverage our precision multi-cavity medical mould experience, balanced runner design and strict process control to supply stable 5ml syringe plunger moulds with consistent cavity-to-cavity quality. Below are key specs, quality control points and manufacturing highlights.
| Centrifuge Tube Mould Cavity Steel | S136 | Recommended Injection Machine | DKM FE Series All-Electric Injection Moulding Machine |
|---|---|---|---|
| Centrifuge Tube Mould Core Steel | S136 | Plastic Material | Medical-grade PP |
| Mould Base Standard / Steel | 4Cr13 Pre-hardened Stainless Steel | Ejection System | Stripper |
| Sliders, Inserts, Lifters Steel | High-strength tool steel with surface hardening treatment | Injection Process | High-speed injection, short cycle time, precise temperature control |
| Number of Cavities | 16-72 cavities | Injection Cycle Time | 12-18 seconds |
| Hot Runner System | Fully hot runner system | Mould Manufacturing Lead Time | 65-75 days |
Quality Control Points
Concentricity of disc head & rod Tight concentricity ensures uniform sliding resistance. Cavity-core tolerance ≤±0.02mm, finished concentricity ≤0.01mm to avoid jamming and gasket damage.
Rod surface finish, burr-free Rod directly contacts the gasket. Mould surface Ra≤0.2μm, tightly locked parting line to eliminate micro flash and liquid leakage risk.
Head flatness & thickness consistency Head flatness ≤0.03mm, inter-cavity thickness difference ≤0.02mm for reliable gasket assembly and sealing.
PP shrinkage compensation & dimensional stability Moldflow simulation + closed-loop temperature & multi-stage packing control reduce dimension drift for mass sterile production.
Medical cleanliness & anti-corrosion Melt-contact parts are stainless steel with mirror finish. Optimized venting, easy disassembly & cleaning for cleanroom use.
Manufacturing Highlights
- Precision anti-deflection slender core Dual fixture clamping + wire EDM, core straightness ≤0.008mm with stress relief to prevent deformation.
- Independent balanced cooling per cavity Separate cooling circuit for each cavity, enhanced cooling on thick head area to balance shrinkage and lower internal stress.
- Balanced filling with sequenced gating Symmetric manifold + sequential valve gates. Gates on non-sealing area to reduce weld lines and equalize filling.
- Mark-free synchronous ejection Pins evenly arranged on the outer ring of plunger head, synchronized ejection to avoid whitening, sink marks and pin marks.
- Multi-cavity pre-delivery validation Continuous trial moulding, test concentricity, surface finish and assembly performance. Shipment only after all cavities pass leak & jam tests.
Mould Flow Analysis for syringe plunger Moulds
Using Mouldflow analysis, we optimize the filling, packing, and cooling processes of the centrifuge tube mould. The analysis simulates the injection moulding process, optimizing cavity layout, gate positions, and temperature control solutions, ensuring uniform cavity filling and reducing air pockets, warping, and short shots, enhancing the moulding stability of the syringe mould.